Flame RetardantPolycarbonate
The hard power of Flame Retardant Polycarbonate
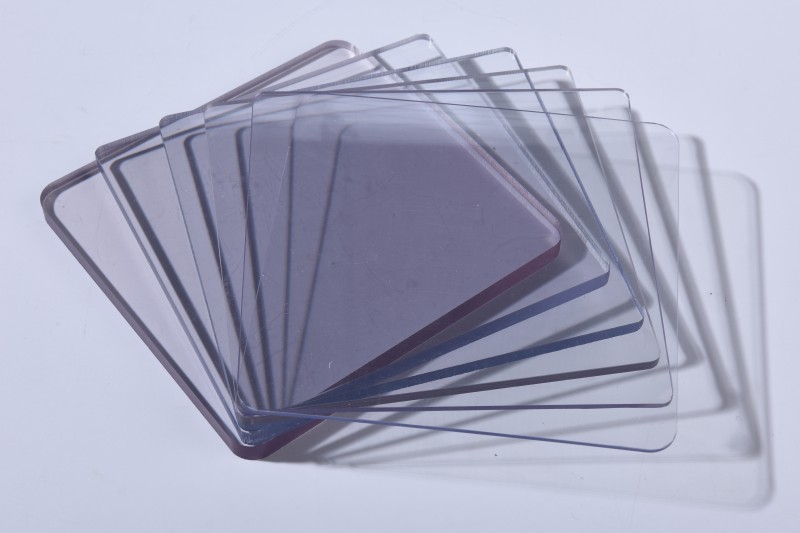
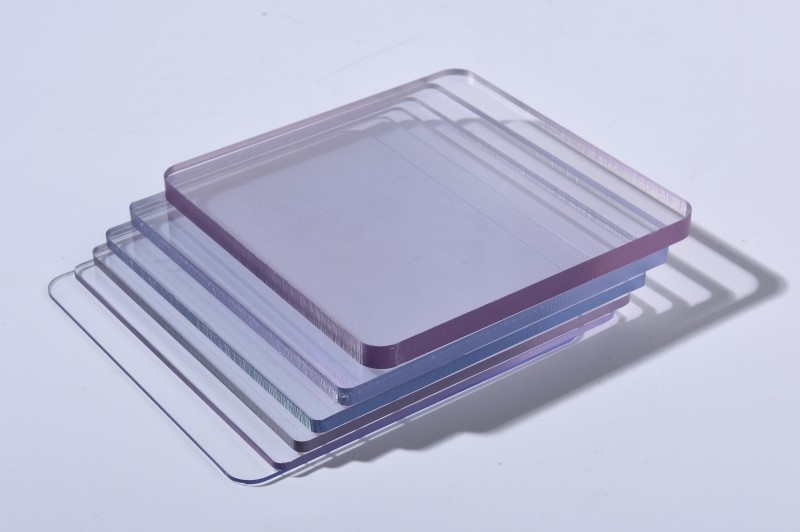
Flame Retardant Polycarbonate
- Flame Retardant Polycarbonate Sheet is 250 times stronger than glass, but half weight;
- It is virtually unbreakable, the right material of window glass;
- It is bullet-proof glass;
- With wide options in colors and surface types, easy to make an eye-catching appearance;
- Co-extruded UV protective layers on one or two sides, the lifespan will be more than 10 years without yellowing;
- Easy to fabricate, flexible, formable and machinable, cold/hot bend, thermoform to shapes;
- Wonderful ink adhesion and print quality;
- Withstands most extreme hot and cold climates between -40°C to 120 °C;
Specification Of Flame Retardant Polycarbonate
| Type | Colors Description |
|---|---|
| Transparent | Clear, Bronze, Brown, Gary, Red, Lighter Blue, Lighter Green |
| Translucent | Black, Opal White, Blue, Green |
| Opaque | Black, Opal White, Yellow, Dark Blue, Red, Dark Grey, Dark Brown |
- Machining Polycarbonate service is available;
- Thin polycarbonate sheet is called polycarbonate films (0.125mm to 0.8mm thickness), and they are available;
| Physical Property | Testing Method | Unit | Value |
|---|---|---|---|
| Specific Gravity | D-792 | g/cm3 | 1.2 |
| Coefficient of Linear Thermal Expansion | D-696 | mm/m °C | 0.065 |
| Thermal Conductivity | C-177 | W/m K | 0.21 |
| Tensile Strength at Yield | D-638 | Mpa or N/mm² | >60 |
| Tensile Strength at Break | D-638 | MPa or N/mm² | >65 |
| Elongation at Break | D-638 | % | >100 |
| Tensile Modulus of Elasticity | D-638 | MPa | 2400 |
| Flexural Strength | D-790 | MPa | 100 |
| Fire rating | UL 94 | / | V2/V0 |
| Fire rating | ASTM E84 | / | Class B or Class A |
| Light transmittance | D-1003 | % | From 80% to 91% |
The default third-party testing organization is SGS;
Flame retardant Polycarbonate Sheet Introduction
Flame Retardant Polycarbonate offers improved fire resistance and heat deflection characteristics over the standard polycarbonate sheet. It meets the flammability codes of the engineering industry, construction industry, and transportation industry, such as UL94, ASTM E84, GB/T2408-2008, UL723, etc. Some people call it Fire Resistant Polycarbonate and Fireproof Plastic.
NAILIPU is the code of NAILIPU Flame Retardant Polycarbonate Sheet, which offers high clarity and surface quality. It is virtually unbreakable with extremely high impact resistance. In the case of fire, flame retardants can reduce the growth of fire in a very short time. As the most popular fire-resistant plastic sheet, flame retardant polycarbonate is the right material for machine guards, industrial parts, electrical components, a wide variety of vehicles, train seats that is requiring flame retardance, and the most application in that glass used.
NAILIPU is a leading supplier of flame-retardant polycarbonate in China. Sometimes, we make flame-retardant polycarbonate with custom colors, such as grey, brown, black, red, etc.
| hickness (mm) | Width (mm) | Length (m) | Packaged as Panel | Packaged as Roll |
|---|---|---|---|---|
| 0.125mm | 1220 | 2.44, 400 | ok | ok |
| 0.175mm | 1220 | 2.44, 350 | ok | ok |
| 0.25mm | 1220 | 2.44, 300 | ok | ok |
| 0.375mm | 1220 | 2.44, 200 | ok | ok |
| 0.5mm | 1220 | 2.44, 150 | ok | ok |
| 0.75mm | 1220 | 2.44, 100 | ok | ok |
| 1mm, 1.5mm | 1000, 1220, 2100, 2650 | 2.44, 5.8, 12, 30, 40 | ok | ok |
| 2mm | 1000, 1220, 2100, 2650 | 2.44, 5.8, 12, 30 | ok | ok |
| 2.5mm, 3mm | 1000, 1220, 2100, 2650 | 2.44, 5.8, 12, 20 | ok | ok |
| 4mm, 5mm, 6mm, 8mm, 10mm | 1000, 1220, 2100, 2650 | 2.44, 5.8, 12 | ok | |
| 8mm, 10mm, 12mm, 15mm | 1000, 1220, 2100, 2650 | 2.44, 5.8, 12 | ok | |
| 16mm, 18mm, 20mm | 1000, 1220, 2100 | 2.44, 5.8 | ok |
Polycarbonate skylight
Skylight roof panel
Transportation system
Aircraft interior component
Reliable Quality: We use advanced production equipment and a strict quality‑control system.
Large Capacity: Eight production lines give an annual output of 50 000 tons.
Proven Experience: We have more than twenty years of manufacturing and export history.
Responsive Service: Dedicated staff reply quickly and follow each order through delivery.
Warranty: We provide a five‑ to ten‑year product warranty.
Performance: Our sheets offer high impact resistance, good bendability, high light transmission, self‑extinguishing fire performance, low weight, sound insulation, anti‑drip surfaces, UV blocking, energy savings, and recyclability.
Frequently Asked Questions
Q: What are the typical flame retardant mechanisms of flame retardant polycarbonate (FR-PC), and how do they differ from halogenated and non-halogenated formulations?
A: FR-PC mainly relies on three mechanisms: ① Condensation charring (PC itself forms a dense carbon layer under high temperature to block heat and oxygen); ② Gas-phase flame inhibition (halogenated formulations release halogen radicals to capture free radicals in the combustion chain, while non-halogenated ones release inert gases like CO₂/H₂O to dilute combustibles); ③ Heat absorption and cooling (additives like metal hydroxides decompose endothermically). The key difference is that halogenated FR-PC has higher flame retardant efficiency but may release toxic gases (e.g., dioxins) during combustion, while non-halogenated ones are more environmentally friendly but often require higher additive loading, which may affect mechanical properties.
Q: How does the addition of flame retardants affect the mechanical properties (tensile strength, impact strength, flexural modulus) of polycarbonate, and what modification methods can mitigate the negative impact?
A: Flame retardants (especially inorganic ones like Mg(OH)₂) usually reduce PC’s mechanical properties: tensile strength may decrease by 10-25%, notched impact strength by 15-30%, and flexural modulus may increase slightly (due to rigid additives). Mitigation methods include: ① Using reactive flame retardants (e.g., phosphorus-containing monomers) that copolymerize with PC to avoid phase separation; ② Adding compatibilizers (e.g., maleic anhydride-grafted POE) to improve interfacial adhesion between flame retardants and PC matrix; ③ Controlling flame retardant particle size (nano-scale additives have less impact on mechanical properties).
Q: What are the key test standards for evaluating the flame retardancy of FR-PC, and what do the typical ratings (e.g., UL94 V-0, V-1, V-2) represent?
A: Core standards include: ① UL94 (Vertical Burning Test, most widely used for plastics); ② IEC 60695 (equivalent to UL94, adopted in the EU); ③ ASTM D635 (Horizontal Burning Test, for materials with low flame retardancy). UL94 ratings are defined by flame duration and dripping: – V-0: After removing the ignition source, flame extinguishes within 10 seconds, no dripping that ignites cotton; – V-1: Flame extinguishes within 30 seconds, no dripping that ignites cotton; – V-2: Flame extinguishes within 30 seconds, but dripping may ignite cotton. For FR-PC used in electrical appliances, V-0 is the most common requirement.
Q: Can FR-PC maintain its flame retardancy and mechanical properties under long-term exposure to high temperatures (e.g., 80-120°C) or UV radiation? What aging resistance improvements are available?
A: Long-term high-temperature exposure (above Tg of PC, ~150°C) causes thermal oxidation of PC chains and volatilization of flame retardants, leading to 10-20% loss of flame retardancy (e.g., UL94 rating drops from V-0 to V-1) and 15-30% decrease in impact strength. UV radiation (280-400 nm) breaks PC’s aromatic rings, resulting in yellowing and reduced tensile strength. Improvements: ① Add heat stabilizers (e.g., phosphite esters) to inhibit thermal oxidation; ② Use UV absorbers (e.g., benzotriazoles) or hindered amine light stabilizers (HALS) to block UV damage; ③ Adopt surface coating (e.g., SiO₂ film) to isolate heat and UV.
Q: What are the limitations of FR-PC in high-voltage electrical applications (e.g., 10kV+), and how to optimize its electrical insulation and arc resistance?
A: Limitations include: ① High-temperature breakdown (PC’s volume resistivity decreases from 10¹⁶ Ω·cm to 10¹² Ω·cm at 120°C, increasing leakage current); ② Poor arc resistance (UL746A arc resistance ≤ 120s, easy to form carbonized channels under arc). Optimization methods: ① Blend with high-insulation resins (e.g., polyphenylene oxide, PPO) to increase volume resistivity to 10¹⁷ Ω·cm; ② Add arc-resistant additives (e.g., alumina trihydrate, ATH) to extend arc resistance to 180s+; ③ Modify the surface (e.g., plasma treatment) to reduce surface leakage current.
Q: How do the smoke density and toxic gas emission of FR-PC compare to other flame retardant plastics (e.g., FR-ABS, FR-PP) during combustion? What measures can reduce smoke and toxicity?
A: FR-PC has lower smoke density than FR-ABS (ASTM E662 specific optical density at 4min: FR-PC ~50 vs. FR-ABS ~120) because PC’s charring mechanism reduces volatile organics. Toxic gas emission: FR-PC (especially non-halogenated) releases less toxic gases (CO, HCl) than halogenated FR-ABS (HCl emission ~500 mg/g vs. FR-PC <50 mg/g). 降烟降毒措施:① Add smoke suppressants (e.g., molybdenum trioxide) to reduce smoke density by 30-40%; ② Use nitrogen-phosphorus synergistic flame retardants (instead of halogen) to cut toxic gas emission by 60-80%; ③ Incorporate carbon nanotubes (CNTs) to form a compact char layer, inhibiting smoke and gas release.
Q: What is the melt flow rate (MFR) range of FR-PC suitable for injection molding, and how does flame retardant content affect MFR? How to adjust processing parameters to avoid defects (e.g., warpage, shrinkage)?
A: Suitable MFR (300°C/1.2kg, ASTM D1238) for injection molding is 5-20 g/10min. Flame retardant content (usually 5-15 wt%) has a dual effect: ① Inorganic flame retardants (e.g., ATH) increase melt viscosity, reducing MFR by 15-30%; ② Reactive phosphorus flame retardants may slightly plasticize PC, increasing MFR by 5-10%. Process adjustment for defects: ① Warpage: Increase mold temperature (80-120°C) to reduce internal stress; use uniform wall thickness design. ② Shrinkage: Increase holding pressure (60-80 MPa) and holding time (5-10s); lower melt temperature (280-310°C) to reduce post-shrinkage. ③ Jetting: Increase injection speed (50-80 mm/s) or use a hot runner system.
Q: Can FR-PC be recycled, and what are the challenges in mechanical recycling (e.g., multiple reprocessing cycles)? How to improve the recyclability of FR-PC products?
A: FR-PC is recyclable, but mechanical recycling faces challenges: ① Flame retardant degradation (e.g., halogenated flame retardants decompose at 280+°C, releasing toxic gases and reducing flame retardancy); ② Chain scission of PC (multiple reprocessing cycles reduce molecular weight, leading to 20-30% lower impact strength). Recyclability improvements: ① Use thermally stable flame retardants (e.g., cyclic phosphorus esters) that withstand 300+°C; ② Add chain extenders (e.g., diisocyanates) during recycling to repair broken PC chains, restoring MFR and mechanical properties by 80-90%; ③ Design products with single-material composition (avoid blending with incompatible resins like ABS) to simplify sorting and recycling.
Q: What are the differences in flame retardant performance and application scenarios between FR-PC and FR-PC/ABS alloys? Why is FR-PC/ABS more widely used in automotive interior parts?
A: Performance differences: ① Flame retardancy: FR-PC has higher UL94 rating (e.g., V-0 at 1.6mm) than FR-PC/ABS (usually V-0 at 3.2mm) because ABS’s butadiene segment is flammable. ② Impact strength: FR-PC/ABS has better low-temperature impact strength (-30°C impact strength ~20 kJ/m² vs. FR-PC ~12 kJ/m²) due to ABS’s rubber phase. Application scenarios: ① FR-PC: Electrical appliance housings (e.g., socket shells), LED light covers (high transparency and heat resistance). ② FR-PC/ABS: Automotive interior parts (e.g., instrument panels, door handles) – reason: it balances flame retardancy (meets FMVSS 302, horizontal burning rate ≤100 mm/min), low-temperature impact resistance (adapts to cold environments), and processability (lower melt temperature than FR-PC, reducing molding energy consumption).
Q: What are the emerging flame retardant technologies for FR-PC (e.g., bio-based flame retardants, nanocomposites), and what are their current technical maturity and commercialization barriers?
Your Trusted Partner for Polycarbonate Products in China
Click on the button, you will find the Trustworthy Supplier Of Polycarbonate Sheet/Acrylic Sheet/Film or Machining services.